

In today’s textile and material manufacturing industries, product quality is measured not only by appearance and durability but also by functional performance. One of the most critical characteristics of fabrics and industrial materials is Air Permeability which determines how easily air can pass through a material. Accurate measurement of this property is essential for manufacturers producing sportswear, medical textiles, filtration materials, protective clothing, and many other products.
To achieve reliable results, laboratories and quality control departments rely on an advanced Air Permeability Tester. This specialized instrument helps manufacturers evaluate fabric breathability and ensure compliance with international testing standards.
What Is Air Permeability?
Air Permeability refers to the rate of airflow passing through a material under specified pressure conditions. A higher Air Permeability Value generally indicates better breathability, making the material more comfortable for clothing applications. Conversely, lower permeability may be desirable for protective garments, filtration products, or wind-resistant fabrics.
Understanding this property helps manufacturers optimize product performance while maintaining consistency in production processes.
Importance of Air Permeability Testing
Modern consumers expect textiles to offer comfort, protection, and functionality. As a result Air Permeability Testing has become an essential step in quality assurance. The testing process allows manufacturers to:
- Evaluate fabric breathability.
- Compare different textile structures.
- Ensure compliance with industry standards.
- Improve product performance.
- Support research and development activities.
By conducting regular tests, companies can identify production variations and make necessary adjustments before products reach the market.
Role of an Air Permeability Tester
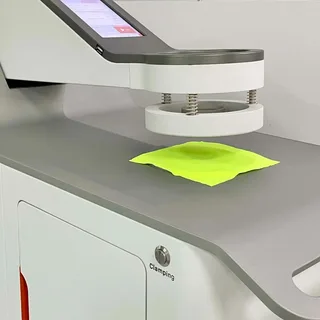
An Air Permeability Tester for Fabric is designed to measure the airflow passing through textile materials under controlled conditions. The instrument creates a pressure difference across the specimen and calculates the amount of air flowing through the test area.
A high-quality Air Permeability Tester for Textile provides precise and repeatable measurements, helping manufacturers maintain strict quality standards. These testing systems are widely used in textile mills, research institutions, inspection laboratories, and educational facilities.
Features of a Modern Permeability Tester
A modern Permeability Tester incorporates advanced technologies to improve testing efficiency and accuracy. Common features include:
- Digital control systems.
- Automatic pressure regulation.
- User-friendly touchscreen interfaces.
- Real-time data recording.
- Compliance with international testing standards.
- Multiple test area options.
Such capabilities make the instrument an indispensable tool for material evaluation and quality management.
Understanding the Air Permeability Method
The Air Permeability Method typically involves securing a specimen over a testing head and applying a specified pressure difference. Air is drawn through the material, and the airflow rate is measured. The resulting data provides an accurate representation of the material’s permeability characteristics.
This standardized testing approach ensures consistency across laboratories and enables manufacturers to compare products effectively.
Benefits of Using an Air Permeability Testing Machine
A professional Air Permeability Testing Machine delivers several advantages for manufacturers and testing laboratories. These include:
Improved Product Quality
Precise testing helps manufacturers develop fabrics that meet specific performance requirements and customer expectations.
Enhanced Process Control
Continuous monitoring of permeability characteristics allows production teams to detect inconsistencies early and implement corrective actions.
Regulatory Compliance
Many industries require documented testing results. A reliable Permeability Testing Machine supports compliance with international standards and certification requirements.
Increased Customer Satisfaction
Products with verified breathability and performance characteristics are more likely to meet user expectations and strengthen brand reputation.
Applications across Industries
An Air Permeability Test Apparatus is used in a wide range of sectors, including:
- Textile manufacturing.
- Medical and healthcare products.
- Automotive materials.
- Technical textiles.
- Filtration systems.
- Protective clothing.
- Nonwoven fabrics.
Because airflow characteristics influence comfort, safety, and functionality, testing remains an important part of product development and quality control.
Choosing the Right Air Permeability Test Equipment
Selecting suitable Air Permeability Test Equipment requires consideration of several factors, including testing standards, specimen types, automation requirements, and reporting capabilities. Manufacturers should choose systems that offer reliable performance, ease of operation, and long-term durability.
For organizations seeking advanced testing solutions, the Air Permeability Tester available at https://chiuvention.com/product/air-permeability-tester provides a comprehensive solution for accurate material evaluation and quality assurance.
Understanding Air Permeability Tester Price
When evaluating testing equipment, the Air Permeability Tester Price is often a key consideration. Pricing may vary depending on automation features, testing range, software capabilities, and compliance requirements. While budget is important, investing in a high-quality instrument often delivers greater value through improved accuracy, efficiency, and long-term reliability.
Conclusion
As performance requirements continue to evolve across textile and industrial applications, accurate Air Permeability Testing has become increasingly important. By utilizing a reliable Air Permeability Tester for Fabric or Air Permeability Tester for Textile manufacturers can measure airflow characteristics with confidence, maintain product consistency, and meet international quality standards.
Whether used in research laboratories or production environments, a modern Air Permeability Testing Machine provides the precision and efficiency needed to evaluate material breathability and ensure superior product performance. With advanced Air Permeability Test Equipment companies can make informed decisions, improve manufacturing processes, and deliver products that meet the highest expectations for quality and functionality.
